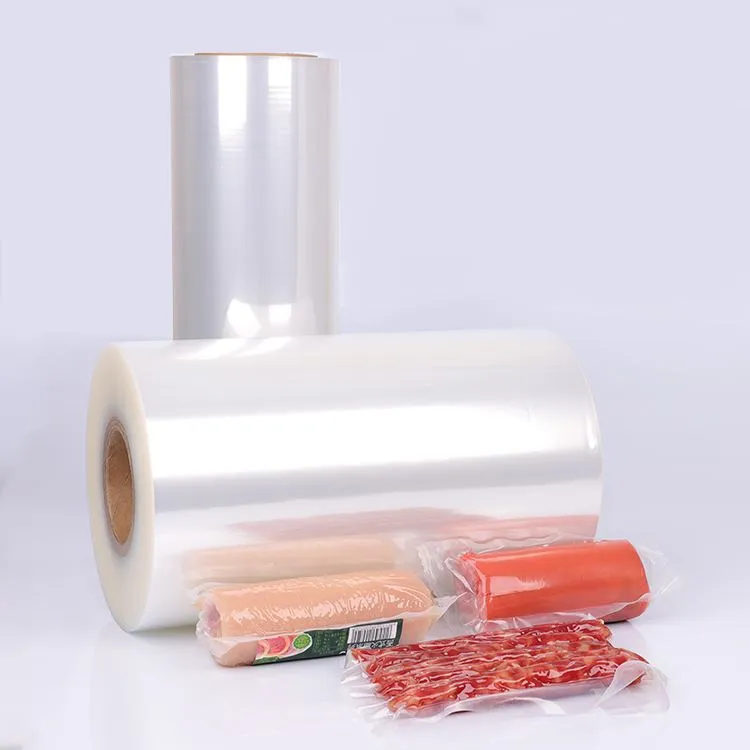
EVOH high-barrier film is a packaging film with ethyl-vinyl alcohol copolymer as the main barrier material. Its outstanding feature is the low permeability of oxygen, coupled with excellent transparency, processing performance and suitability for food packaging, so it is widely used in products that require excellent oxygen barrier performance.
The market for high-performance packaging materials continues to grow, driven by technological advancements in food preservation, pharmaceutical packaging, lightweight packaging, and high-barrier flexible packaging. The application of EVOH high-barrier films is expected to expand further, especially in the context of the need to reduce reduced oxygen permeation, extended shelf life, and enhanced product protection.
1.Food packaging remains a major application area
Food packaging is a key application area of EVOH high-barrier films. Meat, dairy, deli items, cheese, coffee, snacks and certain flavored foods are exposed to oxygen during storage, leading to oxidation, discoloration and flavor degradation.
EVOH has excellent resistance to oxygen and acts as a barrier layer in multi-layer packaging structures, effectively slowing the rate at which oxygen enters the packaging.
For foods with a long shelf life, high barrier packaging helps minimize the impact of the external environment on the product. Therefore, with the growth of cold chain, prepared and ready-to-eat food markets, EVOH films remain to have great potential in food packaging applications.
2.Growing Demand for vacuum packaging and Modified atmosphere packaging
Vacuum packaging and modified atmosphere packaging require high barrier properties of packaging materials. It is essential to maintain a relatively stable internal gas environment; continuous ingress of external oxygen affects the colour, aroma and overall condition of the food.
EVOH high barrier membrane is the core barrier layer of the multilayer composite membrane used to package meat products, seafood, cheese and other foods that require controlled oxygen environments.
Under the background of rapid development of fresh and prepackaged food sectors, enterprises pay attention not only to packaging aesthetics, but also to barrier performance, sealing integrity and processing efficiency. Therefore, combining EVOH with materials such as PE and PP to form multi-layer packaging structures has become a common application method. Huge potential in Pharmaceutical and medical packaging
3.Pharmaceutical products require high stability and protective ability of packaging materials, especially those sensitive to oxygen, which require excellent barrier properties.
EVOH can be used as a barrier layer for drugs or medical packaging to reduce oxygen permeation and create a more stable environment for products. Specific applications require material selection and validation based on drug characteristics, packaging formats and related regulatory requirements.
With the increasing demand for safety, stability and material performance of drug packaging, the application of high barrier film in drug packaging, compound packaging and some medical products is likely to increase.
4. Packaging of household chemicals and personal care products
Cosmetics, skincare products, toiletries and various personal care items also require to be protected by external environmental factors during storage.
For products that are susceptible to oxidation or require special barrier performance, a multi-layer packaging structures with an an EVOH barrier layer may be employed to enhance protection of oxygen and other external elements.
At the same time, consumers are increasingly looking to packaging for aesthetics, transparency, lightweight design and portability. Compared with traditional high barrier materials, EVOH multi-layer films offer superior barrier performance while providing a more flexible packaging designs.
5. Pet Food & High Barrier Flexible Packaging Market
In recent years, pet food packaging to high performance, portable, professional development. Wet foods, meat, pet food and high-fat products require strict control over oxygen and moisture levels during storage.
EVOH high barrier membranes can be utilized in pet food bags, composite soft packaging and trays, using multiple layers to provide the necessary barrier protection.
In addition, products such as coffee, nuts, meats and cheese have high oxygen blocking properties. With the expansion of high-barrier soft packaging market, EVOH applications are likely to expand beyond traditional food packaging to a wider range of products sensitive to storage conditions.
6. Sustainable lightweight packaging Lightweight Packaging to Drive Technological upgrades
Future development of EVOH high barrier films will focus not only on barrier performance, but also increasingly on material reduction, lightweight, and recyclability. Traditional high-barrier packaging tends to rely on thicker composite structures, and EVOH, along with other polymers, acts as a thinner functional barrier layer in a multilayer structure, reducing the usage of materials while meeting performance requirements.
Future industry trends will increasingly focus on EVOH applications in mono-material systems, recyclable packaging structures, downloading (thinning) packaging, and more. However, actual recyclability and structural choices depend on local recycling infrastructure, material combinations and specific packaging designs; it cannot simply be assumed that all packaging containing volatile organic compounds is directly recyclable.
For packaging manufacturers, the future focus is likely to be on striking a balance between oxygen barrier performance, mechanical strength, thermalsealing performance, material usage and sustainability by optimizing EVOH content, membrane structure and processing technology.


Frequently Asked Questions
1. What do EVOH high barrier membranes mainly block?
EVOH is known for its excellent oxygen barrier properties; therefore, it is primarily used in packaging applications that are essential for controlling oxygen permeation.
2. Is EVOH high barrier film suitable for food packaging?
Yes. ' EVOH is often used in multi-layered structure of food packaging; however, the suitability of a particular product for food exposure must be verified in accordance with material composition, manufacturing process and relevant regulations of the target market.
3. Can EVOH high barrier films be used in vacuum packaging?
They can be used in certain types of vacuum packaging. In practical application, the the film's mechanical strength, thermalsealing performance, puncture resistance and specific types of packaged food need to be comprehensively evaluated.