Introduction of EVOH film.
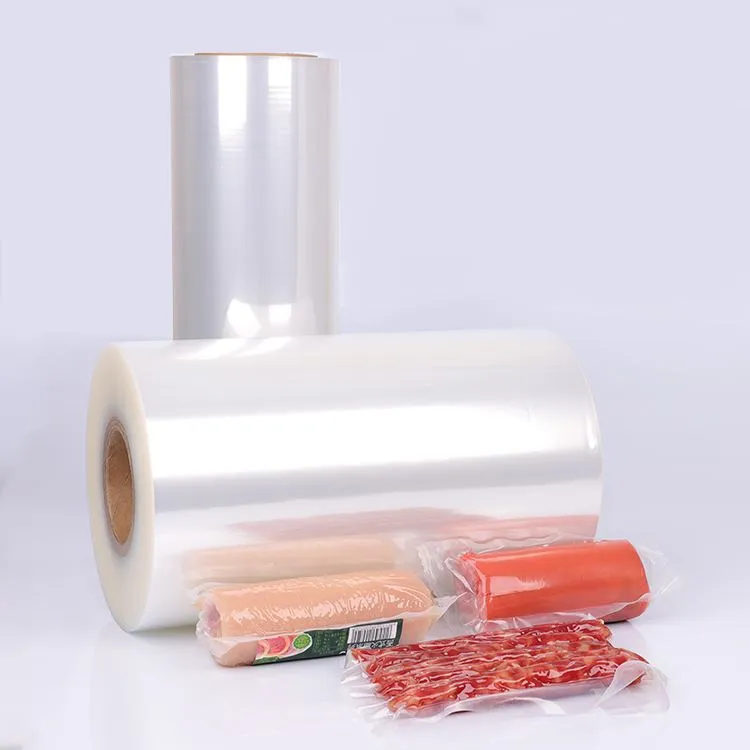
EVOH film, also known as ethylene vinyl alcohol copolymer film, are high performance functional barrier material. EVOH is widely used in food packaging, pharmaceutical packaging, automotive industry, pipe systems and other fields because of its extremely low oxygen permeability, good transparency, printing adaptability and chemical resistance.
In the plastic packaging industry, EVOH is often used not as a primary packaging material alone, but as a functional barrier layer in multi-layer composite packaging structures. For example, adding a layer of EVOH between PE (polyethylene), PP (polypropylene), PA (nylon) and other materials can significantly improve the overall barrier performance of packaging, allowing products to have longer storage periods.
2. Core performance advantages of EVOH film.
1.Excellent oxygen barrier performance
EVOH is best characterized by its high oxygen barrier performance.
Oxygen causes fat oxidation, changes in color, and decreases nutrients in foods, as well as affecting the stability of medications and cosmetics. Ordinary polyethylene and polypropylene plastics have good processing properties, but oxygen permeates easily, and EVOH can effectively prevent oxygen molecules from entering the packaging.
As a result, EVOH is a key material in products that require long-term preservation and quality maintenance.
For example:
Packaging of Meat product can reduce oxidation discoloration.
Cheese packaging prevents mold growth.
Coffee packaging keeps the aroma going
Drug packaging improves stability.
2. Excellent ability to fragrance retention;
In addition to blocking oxygen, EVOH also blocks odor molecules.
Many aromatic ingredients in food are volatile. If the packaging barrier performance is inadequate, the fragrance will gradually dissipate, the external odor will enter the packaging.
EVOH is therefore widely used to:
Coffee bean packaging
Tea packaging;
Seasoning packaging;
Pet food packaging
High-end soft food packaging.
It helps the product retain its original flavor and enhance consumer experience.
3. High transparency
EVOH has better transparency than conventional barrier materials.
Transparent packaging allows consumers to see the product directly and improves presentation. For example:
Fresh meat;
Cheese;
Cooked Food;
Frozen food.
The combination of high transparency and high barrier gives EVOH a distinct advantage in the field of high-end food packaging field.
4. Good processing performance;
EVOH can be produced through a variety of plastic processing methods, including:
Co-extrusion blown film;
Casting film production;
Multi-layer composite;
Thermal molding.
multi-layer co extrusion technology is usually used, with EVOH as intermediate barrier layer.
Typical structure:
PE / EVOH / PE
Of which:
PE has flexibility and heat sealing performance.
EVOH has barrier properties.
You can also use:
PA / EVOH / PE
For packaging with high mechanical strength requirements.
3. Main application fields of EVOH membrane.
1. Food packaging industry
Food packaging is EVOH's largest application market.
(1) Meat packaging
Includes:
meat vacuum;
Ham wrap
Sausage wrappers
Packaging of cooked meat products.
Meat is susceptible to oxygen, causing color changes and spoilage, and therefore requires high barrier materials.
EVOH film reduce oxygen access and extend the shelf life of refrigerated products.
(2) Dairy product packaging
For example:
Cheese packaging
Butter wrap
Dairy product containers.
Cheese and other products are highly sensitive to oxygen and water and require a stable packaging environment.
EVOH reduces the risk of oxidation and microbial growth.
(3) Coffee, tea, nut packaging.
These products usually have a high economic value and a high incense retention requirement.
EVOH can:
To prevent the loss of fragrance;
Prevent external oxygen from entering;
Keep the product fresh.